
Delivery Management Fundamentals
納期管理基礎
Production Management Operations Grade 3 生産管理オペレーション (BC検定) · ビジネス・キャリア検定 生産管理オペレーション3級 · Written by Tokutei Pass based on the official study texts; not copied verbatim.
1. 納期管理の意義・納期遅れの弊害と「早期納入の弊害」
1. Significance of Delivery Management, Harm of Late Delivery, and "Harm of Early Delivery"
「納期」とは、顧客や後工程から指定された「要求納期」に対し、生産能力や資材の調達状況を確認したうえで合意・約束した「契約納期(回答納期)」のことです。「納期管理」とは、約束した期日に約束した場所へ指定の品物と数量を確実に納めるための管理活動です。
"Delivery date (Nouki)" refers to the "Contracted (Promised) Delivery Date" agreed upon after verifying production capacity and material availability against the "Requested Delivery Date" specified by the customer or downstream process. "Delivery Management" is the control activity ensuring that the specified items and quantities are reliably delivered to the promised place on the promised date.
「納期遅れ(納期遅延)」を引き起こすと、顧客の生産ラインを止めてしまい社会的信用を失墜させるだけでなく、違約金の発生・次回以降の失注・特急手配や残業によるコスト増大など重大な損失を招きます。
Causing a "Delivery Delay (late delivery)" not only halts the customer's production line and destroys corporate credibility, but also triggers severe losses such as penalty fees, lost future orders, and surging costs from expedited shipping and overtime work.
一方、「遅れなければ早く納めるほど良い」というのは誤りです。指定された納期より早く造りすぎたり早く納入したりする「早期生産・早期納入」にも大きな弊害があります。
On the other hand, the belief that "as long as it's not late, the earlier we deliver the better" is mistaken. Producing or delivering earlier than the specified due date—"Early Production / Early Delivery"—also causes serious harm.
早期生産・早期納入を行うと、納入先や自社の倉庫スペースを圧迫し、在庫保管費の増加・資金の早期固定化(運転資金の悪化)・設計変更時の手直しロスを招くほか、本当に急ぐべき他の製品の生産を遅らせる原因になります。納期は「遅すぎず、早すぎず(ジャスト・イン・タイム)」が鉄則です。
Early production and early delivery squeeze warehouse space at both the customer's site and your own plant, increase inventory holding costs, tie up working capital prematurely, cause rework losses if design changes occur, and delay the production of other items that are genuinely urgent. The ironclad rule of delivery is "Neither too late nor too early (Just-In-Time)."
Key points
- 納期管理=顧客の「要求納期」と自社の生産能力を調整して決めた「契約納期」を厳守し、生産リードタイムの短縮を図る活動。
Delivery Management = strictly meeting the "Contracted Delivery Date" (reconciled between the customer's "Requested Delivery Date" and plant capacity) while shortening production lead time. - 納期遅れの弊害=顧客からの信用失墜・違約金や損害賠償・失注・残業や特別輸送による原価高騰。
Harm of Late Delivery = loss of customer trust, penalty charges/damages, lost orders, and cost spikes from overtime and special transport. - 早期生産・早期納入の弊害=保管場所の圧迫・在庫維持費の増大・資金繰りの悪化・設計変更時の不良化・他製品の納期圧迫。
Harm of Early Production / Early Delivery = cramped storage space, higher inventory carrying costs, worsened cash flow, obsolescence/rework upon design changes, and delaying other urgent products.
| Word | Meaning |
|---|---|
| 要求納期と契約納期 | Requested Delivery Date and Contracted Delivery Date |
| 納期遅延の弊害 | harm of delivery delays |
| 早期生産・早期納入の弊害 | harm of early production and early delivery |
| ジャスト・イン・タイム(遅すぎず早すぎず) | Just-In-Time (neither too late nor too early) |
2. 生産形態別(見込生産と受注生産)の納期管理の特徴
2. Delivery Management Characteristics by Production Type (Make-to-Stock vs. Make-to-Order)
納期管理の重点は生産形態によって大きく異なります。まず「見込生産(少品種多量の連続生産)」では、完成品在庫から直ちに出荷するため、顧客への納入リードタイムが極めて短いのが特徴です。
The focus of delivery management differs greatly depending on the production type. First, in "Make-to-Stock Production (low-mix high-volume continuous production)," products are shipped immediately from finished-goods inventory, making the delivery lead time to the customer extremely short.
そのため見込生産の納期管理では、高精度な「需要予測」と適切な「安全在庫の設定(欠品防止)」、および工場内で計画生産量を毎日遅れなく平準化して造り続ける「進捗管理(流動数曲線など)」が中心となります。
Therefore, delivery management in make-to-stock production centers on high-accuracy "Demand Forecasting," setting appropriate "Safety Stock (preventing stockouts)," and "Progress Control (using cumulative flow curves, etc.)" to maintain leveled daily production without falling behind.
これに対し、「受注生産(多品種少量の個別・ロット生産)」では、注文を受けてから設計・資材調達・製造を開始するため、受注から納入までの全リードタイムがそのまま納期に直結します。
In contrast, in "Make-to-Order Production (high-mix low-volume individual or lot production)," design, material procurement, and manufacturing begin only after an order is received, so the entire cumulative lead time from order receipt to shipment directly determines the delivery date.
したがって受注生産の納期管理では、製造部門だけでなく「営業→設計→生産計画→資材購買→製造→検査・出荷」という全部門のリードタイム短縮と、個別注文ごとの「日程管理・余力管理(ガントチャートなど)」が最重要となります。
Consequently, delivery management in make-to-order production places top priority on shortening lead times across all departments—"Sales → Design → Production Planning → Purchasing → Manufacturing → Inspection & Shipping"—together with order-by-order "Schedule Control and Capacity Control (using Gantt charts, etc.)."
Key points
- 見込生産の納期管理=需要予測の精度向上・適正な製品在庫の維持(品切れ防止)・一定ペースの連続生産維持が重点。
Make-to-Stock Delivery Management = focuses on improving demand forecast accuracy, maintaining proper finished-goods inventory (preventing stockouts), and sustaining steady continuous output. - 受注生産の納期管理=設計・購買・製造・出荷の「全工程リードタイムの短縮」と注文ごとの「個別進捗・余力管理」が重点。
Make-to-Order Delivery Management = focuses on "shortening total lead time across all departments" (design, purchasing, manufacturing, shipping) and "individual order progress/capacity control." - 受注生産では、製造現場に入る前の「設計の出図遅れ」や「資材の入荷遅れ」が納期遅延の最大要因になりやすい。
In make-to-order production, "late drawing release from Design" or "late material arrival" before work even reaches the shop floor easily becomes the biggest cause of delivery delays.
| Word | Meaning |
|---|---|
| 見込生産の納期管理(欠品防止・需要予測) | Make-to-Stock delivery management (stockout prevention and demand forecasting) |
| 受注生産の納期管理(全部門リードタイム短縮) | Make-to-Order delivery management (company-wide lead time reduction) |
| 調達・設計・製造リードタイム | procurement, design, and manufacturing lead times |
3. 部門別の納期遅れ原因と対策①(設計部門・生産計画部門)
3. Delivery Delay Causes and Countermeasures by Department ① (Design & Production Planning)
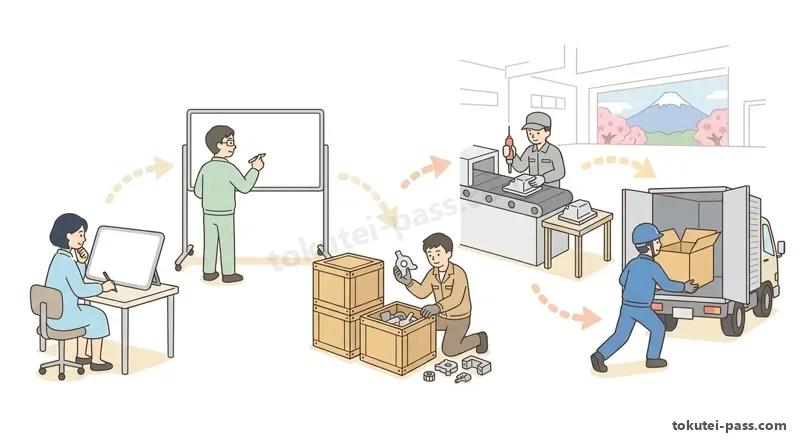
納期遅れは工場の現場だけでなく、上流から下流までの5つの部門それぞれに原因と対策があります。第1の「設計部門」における遅れの原因は、顧客との仕様打合わせの遅れ、図面や部品表の「出図遅れ」、図面ミスによる頻繁な「設計変更」、特殊部品の多用などです。
Delivery delays originate not only on the shop floor but across five departments from upstream to downstream. First, in the "Design Department," causes of delay include slow specification finalization with customers, "late drawing/BOM release (Shutsuzu okure)," frequent "engineering design changes" due to drawing errors, and overuse of custom non-standard parts.
設計部門の対策としては、①部品の「標準化・共通化(モジュール化)」と過去図面の流用、②3次元CADの活用、③設計段階から製造・購買部門と協力して同時並行で開発を進める「コンカレントエンジニアリング」と「デザインレビュー(DR:設計審査)」の徹底が有効です。
Countermeasures in the Design Department include: ① "Part standardization and commonality (modularization)" and reusing past drawings, ② Utilizing 3D CAD, and ③ Thoroughly implementing "Concurrent Engineering" (collaborating simultaneously with manufacturing and purchasing from the design stage) and "Design Reviews (DR)."
第2の「生産計画(工程管理)部門」における原因は、現場の真の生産能力(余力)を無視した無理な日程計画、営業からの無秩序な「飛び込み特急注文」による現場の混乱、手配漏れやリードタイム見積ミスです。
Second, in the "Production Planning (Process Control) Department," causes include unrealistic schedules that ignore actual shop-floor capacity, shop-floor chaos caused by disorderly "rush / drop-in orders" from sales, ordering omissions, and lead-time estimation errors.
生産計画部門の対策としては、①正確な標準時間と工程能力の把握、②「山積み・山崩し」による負荷の平準化とボトルネック工程への対策、③営業・製造との定期的な「生産会議(生販調整)」と飛び込み注文の受付ルール化を行います。
Countermeasures in the Production Planning Department include: ① Accurately grasping standard times and process capabilities, ② Leveling workloads via "Load Piling and Load Leveling (Yamazumi / Yamakuzushi)" and resolving bottleneck processes, and ③ Holding regular "Production-Sales Coordination Meetings" and establishing clear rules for accepting rush orders.
Key points
- 設計部門の原因=出図遅れ・設計変更の多発/対策=部品の標準化・共通化、デザインレビュー(DR)、コンカレントエンジニアリング。
Design Dept causes = late drawing release, frequent design changes / Countermeasures = part standardization/commonality, Design Review (DR), Concurrent Engineering. - 生産計画部門の原因=現場能力を無視した計画・飛び込み注文の無秩序な投入。
Production Planning Dept causes = scheduling that ignores shop capacity, disorderly insertion of rush orders. - 生産計画部門の対策=余力管理(山積み・山崩し)の徹底、ボトルネック工程の解消、営業との生販調整ルール化。
Production Planning Dept countermeasures = thorough capacity control (load piling & leveling), resolving bottlenecks, and establishing Production-Sales coordination rules.
| Word | Meaning |
|---|---|
| 出図遅れと設計変更 | late drawing release and engineering design changes |
| 部品の標準化・共通化(モジュール設計) | part standardization and commonality (modular design) |
| コンカレントエンジニアリングとデザインレビュー(DR) | Concurrent Engineering and Design Review (DR) |
| 飛び込み注文のルール化と生販調整 | rules for rush orders and Production-Sales coordination |
4. 部門別の納期遅れ原因と対策②(資材購買・製造・物流出荷部門)
4. Delivery Delay Causes and Countermeasures by Department ② (Purchasing, Manufacturing, Logistics/Shipping)
第3の「資材・購買・外注部門」における遅れ原因は、発注手続きの遅れ、帳簿在庫と実在庫の不一致による急な欠品、購入品・外注加工品の納入遅れや受入不良です。
Third, in the "Materials, Purchasing & Subcontracting Department," delay causes include delayed purchase order processing, sudden stockouts due to discrepancies between book and physical inventory, and late delivery or receiving defects from suppliers and subcontractors.
資材・購買部門の対策は、①納期の数日前に事前確認を行う「事前督促(カムアップシステム等)」、②外注先への工程監査や技術指導(不良・遅れ防止)、③リスク分散のための複数社購買(2社発注)やリードタイム短縮です。
Countermeasures in the Purchasing Department include: ① "Advance expediting / follow-up (using a Come-Up System, etc.)" several days before the due date, ② Process audits and technical guidance for subcontractors (preventing defects and delays), and ③ Multi-sourcing (two-supplier ordering) to spread risk and shorten procurement lead time.
第4の「製造部門(職場)」における原因は、設備の突発故障、品質不良による手直し・再製作、段取り替えの長時間化、特定の熟練工しか作業できないことによる欠勤時の停滞などです。
Fourth, in the "Manufacturing Department (Shop Floor)," causes include sudden equipment breakdowns, rework or remaking due to quality defects, lengthy setup/changeover times, and work stoppages when the only skilled worker capable of a task is absent.
製造部門の対策は、①日常保全・予防保全による故障ゼロ化、②ポカヨケと作業標準遵守による不良ゼロ化、③シングル段取り化によるロット縮小、④作業者の「多能工化」による応援体制づくりです。
Countermeasures in the Manufacturing Department include: ① Zero breakdowns through daily and preventive maintenance, ② Zero defects through Poka-yoke and adherence to standard operating procedures, ③ Lot-size reduction via Single-Minute Exchange of Die (Single Setup), and ④ Building flexible backup capability through "Multi-Skilled Workers (Tanoukou-ka)."
第5の「物流・出荷部門」では、ピッキングミス(誤出荷・数量不足)、梱包資材の不足、トラック手配ミスや交通渋滞が原因となるため、バーコード・ハンディターミナル検品による誤出荷防止や出荷計画の早期共有で対策します。
Fifth, in the "Logistics & Shipping Department," causes include picking errors (wrong item shipped or quantity shortage), shortage of packing materials, truck booking mistakes, or traffic delays; countermeasures include barcode/handheld-terminal verification to prevent shipping errors and early sharing of shipping schedules.
Key points
- 資材・購買部門の対策=納期前の「事前督促(カムアップシステム)」、外注先への技術・工程指導、複数社発注。
Purchasing Dept countermeasures = "Advance expediting (Come-Up System)" prior to due dates, technical/process guidance for subcontractors, and multiple-supplier ordering. - 製造部門の対策=予防保全(故障防止)、ポカヨケ(不良・手直し防止)、段取り短縮、多能工化(負荷変動・欠勤への柔軟対応)。
Manufacturing Dept countermeasures = preventive maintenance (no breakdowns), Poka-yoke (no defects/rework), setup time reduction, and multi-skilled workers (flexibility for load shifts and absences). - 物流・出荷部門の対策=バーコード照合等によるピッキングミス・誤出荷の防止、輸送車両の早期手配。
Logistics & Shipping Dept countermeasures = preventing picking/shipping errors via barcode verification and arranging transport vehicles early.
| Word | Meaning |
|---|---|
| 事前督促と外注指導 | advance expediting and subcontractor guidance |
| 多能工化と段取り時間短縮 | multi-skilled workers and setup time reduction |
| 誤出荷(ピッキングミス)防止 | preventing mis-shipments (picking errors) |
5. 納期管理のシステムと手配方式(MRP・POP・VMI・追番・製番管理)
5. Delivery Control Systems and Ordering Methods (MRP, POP, VMI, Seiban & Oiban Control)
納期を確実に守るため、様々な情報管理システムや手配方式が活用されます。「MRP(資材所要量計画)」は、基準生産計画(MPS)と部品表(BOM)・在庫データ・調達リードタイムをもとに、最終製品の納期から逆算(バックワード)して各部品の正味発注量と発注時期を自動計算するシステムです。
Various information systems and ordering methods are used to ensure on-time delivery. "MRP (Material Requirements Planning)" is a system that uses the Master Production Schedule (MPS), Bill of Materials (BOM), inventory data, and procurement lead times to calculate backward from the finished product's due date, automatically determining net order quantities and order release dates for every part.
「POP(生産時点情報管理)」は、工場内の各機械や作業者の端末(バーコードリーダー・タッチパネル・センサー等)から、「いつ・誰が・どのロットを・何個完成させたか」という実績データをリアルタイムに収集し、進捗や遅れを即座に把握するシステムです。
"POP (Point of Production)" is a system that collects real-time shop-floor performance data—"when, who, which lot, and how many units were completed"—directly from machines and worker terminals (barcode readers, touch panels, sensors), enabling instant visibility of progress and delays.
また企業間連携として、サプライヤー(納入業者)側が顧客工場の在庫データや消費状況を共有・監視し、サプライヤー主導で適切なタイミングと数量を自動補充する「VMI(ベンダー主導型在庫管理)」も納期遅れ・欠品防止に威力を発揮します。
In inter-company collaboration, "VMI (Vendor Managed Inventory)"—where the supplier shares and monitors the customer plant's inventory and consumption data to proactively replenish stock at the right time and quantity—is also highly effective in preventing delivery delays and stockouts.
なお伝統的な現場の手配方式には、個別受注の注文ごとに固有の「製造番号(製番)」を付けてすべての部品・工程をひも付け管理する「製番管理」と、連続生産において1個目から順番に通し番号(追番・号口番号)を振ってどこまで進んでいるかを管理する「追番管理」があります。
Traditional shop-floor control methods include "Manufacturing Number Control (Seiban Kanri)," which assigns a unique "Manufacturing Number (Seiban)" to each individual customer order to link and track all parts and processes for that order, and "Sequential Number Control (Oiban Kanri)," which assigns cumulative serial numbers starting from unit #1 in continuous production to track how far production has progressed.
Key points
- MRP(資材所要量計画)=部品表(BOM)・在庫・リードタイムから、製品納期に間に合う部品の発注時期と数量を逆算するシステム。
MRP (Material Requirements Planning) = backward-calculates part order timing and net quantities from BOM, inventory, and lead time to meet finished product due dates. - POP(生産時点情報管理)=製造現場の機械や端末から生産実績・進捗・稼働情報をリアルタイムに収集・管理するシステム。
POP (Point of Production) = collects and manages real-time production results, progress, and machine status directly from shop-floor machines and terminals. - 製番管理=個別受注生産で注文ごとの製造番号により管理/追番管理=見込・連続生産で製品の通し番号(累計番号)により進捗を管理。
Seiban Control = tracks make-to-order production by unique order manufacturing number / Oiban Control = tracks continuous production progress by cumulative sequential unit number.
| Word | Meaning |
|---|---|
| MRP(資材所要量計画) | MRP (Material Requirements Planning) |
| POP(生産時点情報管理) | POP (Point of Production information management) |
| VMI(ベンダー主導型在庫管理) | VMI (Vendor Managed Inventory) |
| 製番管理と追番管理 | Seiban (manufacturing number) control and Oiban (sequential number) control |
6. 納期遅延の問題解決手順(応急対策と恒久対策)
6. Problem-Solving Procedure for Delivery Delays (Emergency Countermeasures vs. Permanent Countermeasures)
万一、工程の遅れや納期遅延が発生(または予測)された場合は、体系的な問題解決手順に従って迅速に対処します。最初に、どの注文・どの工程で何日(何個)遅れているかという「現状の正確な把握」と、顧客・関係部門への速やかな連絡・納期調整を行います。
If a process delay or delivery delay occurs (or is predicted), rapid action is taken following a systematic problem-solving procedure. First, "accurately grasp the current status"—which order and which process is delayed by how many days (or units)—and immediately notify the customer and related departments to coordinate schedule adjustments.
同時に、目の前の遅れを取り戻すための「応急対策(暫定対策)」を直ちに実施します。具体的には、残業や休日出勤、他職場からの応援投入、外注の活用、ロット分割(先行してできあがった分だけ先に後工程や顧客へ送る)、特急便での輸送などです。
Simultaneously, implement immediate "Emergency (Temporary) Countermeasures" to recover the current delay. Specific actions include overtime or holiday work, deploying support workers from other shops, utilizing subcontractors, lot splitting (sending completed partial quantities ahead to the next process or customer), and arranging express transport.
しかし、応急対策だけでは再び同じ納期遅れが繰り返されます。そこで納期遅れのデータを「部門別・製品別・原因別」に層別してパレート図にまとめ、特性要因図や「なぜなぜ分析(5回のなぜ)」を使って表面的な現象ではなく「真の原因(真因)」を突き止めます。
However, emergency measures alone allow the same delays to recur. Therefore, stratify delay data "by department, by product, and by cause" into a Pareto chart, and use a Cause-and-Effect Diagram and "Why-Why Analysis (5 Whys)" to uncover the "True Root Cause" rather than superficial symptoms.
そして真因を根本から断つ「恒久対策(再発防止策)」を実施し、効果を確認したうえで、手配基準や作業標準書・リードタイム設定を見直す「標準化(歯止め)」を行って定着させます。
Then execute "Permanent Countermeasures (Recurrence Prevention)" to eliminate the root cause, verify the effect, and perform "Standardization (Locking-in)" by revising ordering rules, standard operating procedures, and lead-time settings.
Key points
- 納期遅れ発生時は、まず現状を把握して関係部署・顧客へ連絡し、残業・応援・ロット分割などの「応急対策」で遅れを挽回する。
When a delay occurs: first grasp the status, notify related departments & the customer, and recover the delay via "Emergency Countermeasures" (overtime, support staff, lot splitting). - 次に遅れデータを部門別・原因別に層別(パレート図)し、なぜなぜ分析や特性要因図で「真因(根本原因)」を特定する。
Next, stratify delay data by department/cause (Pareto chart) and identify the "True Root Cause" using 5-Why Analysis and Fishbone diagrams. - 真因に対する「恒久対策(再発防止)」を行い、効果確認後に業務ルールや作業標準を改定して「標準化」する。
Implement "Permanent Countermeasures (recurrence prevention)" targeting the root cause, confirm effectiveness, and revise work rules/standards for "Standardization."
| Word | Meaning |
|---|---|
| 応急対策(残業・応援・ロット分割) | emergency / temporary countermeasures (overtime, support, lot splitting) |
| 恒久対策(再発防止策) | permanent countermeasures (recurrence prevention) |
| なぜなぜ分析と真因の特定 | Why-Why Analysis (5 Whys) and root cause identification |
| 標準化と管理の定着(歯止め) | standardization and establishing control |
7. 目で見る納期管理ツール①(カムアップシステム・差立盤・アンドン)
7. Visual Delivery Management Tools ① (Come-Up System, Dispatching Board, Andon)
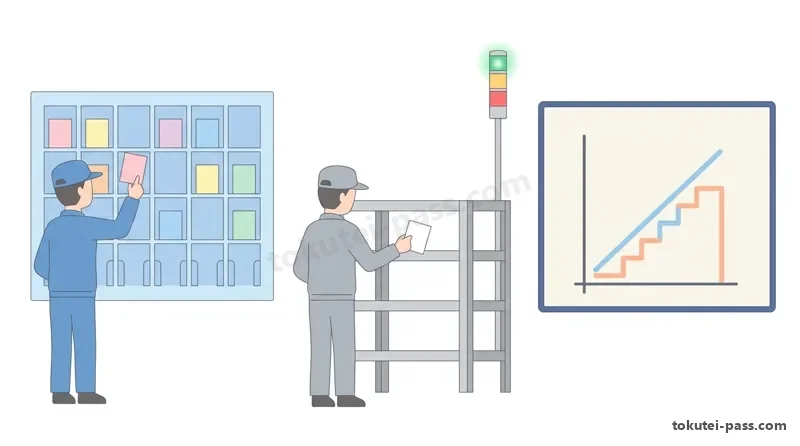
納期遅れを未然に防ぐには、誰が見ても異常や遅れがすぐわかる「目で見る管理(視覚管理)」の道具が有効です。購買品や外注品の納期管理でよく使われる手法が「カムアップシステム」です。
To prevent delivery delays before they happen, "Visual Management (management by sight)" tools that let anyone spot abnormalities or delays at a glance are highly effective. A classic method widely used for managing due dates of purchased and subcontracted parts is the "Come-Up System."
「カムアップシステム」とは、1日から31日までの日付別のポケット(またはボックス)を設けたファイル棚に発注書の控えや納品伝票を「納期(または事前督促日)のポケット」に入れておき、毎日その日のポケットを見ることで、チェックすべき伝票が自動的に浮き上がってくる(カムアップする)仕組みです。
The "Come-Up System" uses a filing rack with dated pockets (or boxes) numbered 1 through 31; copies of purchase orders or delivery slips are placed into the "pocket of the due date (or advance expediting date)," so simply checking today's pocket each morning causes the slips requiring follow-up to automatically "come up" without omission.
また製造現場では、各機械や作業者の作業予定を時間軸に沿ってポケットに差し込み、現在どの作業を行い、次に何をやるか、遅れている伝票はないかを管理する「差立盤(管理盤・ディスパッチングボード)」が活用されます。
On the manufacturing shop floor, a "Dispatching Board (Sashitate-ban / Control Board)" slots work instruction tickets for each machine or operator along a timeline, visually managing what job is currently running, what comes next, and whether any tickets are overdue.
さらに、ラインの目標生産数と現在の実績数・進捗の遅れ・設備異常などを電光表示盤やランプでリアルタイムに表示する「アンドン(行灯)」や「生産管理板」により、1時間ごとの遅れをその場で発見して即座に対処します。
Furthermore, "Andon (illuminated overhead boards)" and electronic "Production Management Boards" display real-time line target counts, actual output, progress delays, and equipment abnormalities via lights and LEDs, allowing hourly delays to be spotted and addressed on the spot.
Key points
- カムアップシステム=発注伝票などを日付別のボックスやファイルに入れておき、督促日や納期が来ると自動的に対象伝票が浮き上がるようにする納期管理法。
Come-Up System = a visual delivery control method that files order slips into date-indexed pockets/boxes so slips requiring follow-up automatically surface before the due date. - 差立盤(管理盤)=作業指示票や現品票を機械別・日付順に並べて差し、作業順序と遅れを視覚管理するボード。
Dispatching Board (Sashitate-ban) = a board that slots work instruction tickets and identification tags by machine and date to visually control job sequence and delays. - アンドン・生産管理板=計画数と現在実績数・ライン異常をランプ等でリアルタイムに表示する目で見る管理道具。
Andon & Production Management Board = visual tools displaying planned quantity, current actual output, and line abnormalities in real time.
| Word | Meaning |
|---|---|
| カムアップシステム(日付別ファイルによる事前督促) | Come-Up System (advance expediting via date-indexed files) |
| 差立盤(管理盤) | Dispatching Board (Sashitate-ban / control board) |
| アンドンと生産管理板 | Andon and Production Management Board |
8. 目で見る納期管理ツール②(ガントチャート・流動数曲線・製造三角図)
8. Visual Delivery Management Tools ② (Gantt Chart, Cumulative Flow Curve, Manufacturing Triangle Chart)
日程と進捗をグラフで視覚化する3大図表が「ガントチャート」「流動数曲線」「製造三角図」です。1つ目の「ガントチャート」は、横軸に時間(日付)をとり、注文や機械ごとに予定と実績を横棒で比較する図で、個別受注生産の進捗管理に最も適しています。
The three major charts that visualize schedules and progress graphically are the "Gantt Chart," "Cumulative Flow Curve," and "Manufacturing Triangle Chart." First, the "Gantt Chart" places time (dates) on the horizontal axis and compares planned vs. actual progress for each order or machine using horizontal bars—best suited for individual make-to-order progress control.
2つ目の「流動数曲線」は、横軸に時間(日付)、縦軸に「累計数量」をとり、累計投入線と累計産出(完成)線を描く図で、縦の差で「仕掛品在庫数」、横の差で「平均滞留日数(リードタイム)」、計画線との差で「生産の進み・遅れ」を把握します。
Second, the "Cumulative Flow Curve" plots time (dates) on the horizontal axis and "cumulative quantity" on the vertical axis, drawing cumulative input and cumulative output (completion) lines; the vertical gap shows "WIP inventory," the horizontal gap shows "average dwell time (lead time)," and deviation from the plan line shows "production lead or lag."
3つ目の「製造三角図」は、流動数曲線を応用して、横軸に「時間(期間)」、縦軸に「生産数量(累計)」をとり、特定ロットの①生産予定線、②材料投入(着手)実績線、③完成(納入)実績線を描き、外枠と合わせて三角形の形に表した図です。
Third, the "Manufacturing Triangle Chart (Seizou Sankakuzu)" adapts the cumulative flow curve by plotting "Time (period)" on the horizontal axis and "Production Quantity (cumulative)" on the vertical axis, drawing ① the Planned Production Line, ② the Actual Material Input (Start) Line, and ③ the Actual Completion (Delivery) Line for a specific lot inside a triangular frame.
製造三角図を見れば、予定期間と予定数量の直角三角形の斜辺(予定線)に対して、着手線や完成線がどのくらい遅れているか、工程内に仕掛品が何個滞留しているか、納期に間に合うペースかどうかが一目で診断できます。
By looking at the Manufacturing Triangle Chart, one can diagnose at a glance how far the start line and completion line lag behind the hypotenuse (planned line) of the right triangle formed by planned period and planned quantity, how many WIP units are backed up in the process, and whether the current pace will meet the delivery date.
Key points
- ガントチャート=横軸に時間をとり、予定と実績を横棒で対比する図(個別生産・ロット生産の進捗管理に最適)。
Gantt Chart = places time on the horizontal axis and contrasts plan vs. actual with horizontal bars (ideal for individual and lot production progress control). - 流動数曲線=累計投入線と累計完成線から「仕掛品数(縦の差)」と「滞留時間(横の差)」を把握する図。
Cumulative Flow Curve = grasps "WIP quantity (vertical gap)" and "lead time / dwell time (horizontal gap)" from cumulative input and cumulative completion lines. - 製造三角図=横軸に時間・縦軸に数量をとり、予定線・着手線・完成線を三角形のグラフに描いて進捗と仕掛状況を視覚化する図。
Manufacturing Triangle Chart = plots time on the horizontal axis and quantity on the vertical axis, drawing Plan, Start, and Completion lines in a triangular graph to visualize progress and WIP.
| Word | Meaning |
|---|---|
| ガントチャート(横棒による予定・実績対比) | Gantt Chart (horizontal bar comparison of plan vs. actual) |
| 流動数曲線(投入累計と完成累計) | Cumulative Flow Curve (cumulative input and cumulative completion) |
| 製造三角図(予定線・着手線・完成線) | Manufacturing Triangle Chart (plan line, start line, completion line) |
試験によく出るポイントと覚え方
High-Frequency Exam Points and Memory Aids
納期管理では、まず「早期納入(早作り・早出し)は良いことではなく、在庫増大・保管スペース圧迫・資金固定化・他製品の遅れを招く弊害がある」という正誤問題が頻出です。
In Delivery Management, true/false questions frequently test the principle that "Early delivery (making or shipping too early) is NOT good—it causes excess inventory, cramped storage space, tied-up capital, and delays to other products."
次に「5つの部門(設計・生産計画・資材購買・製造・物流)ごとの納期遅れ原因と対策」の組み合わせ問題が出ます。「部品標準化・DR=設計部門」「山積み山崩し=生産計画部門」「事前督促=資材購買部門」「段取り短縮・多能工化=製造部門」と整理しましょう。
Next, expect matching questions on "Delivery delay causes and countermeasures across the 5 departments (Design, Production Planning, Purchasing, Manufacturing, Logistics)." Organize them clearly: "Part standardization & DR = Design," "Load piling & leveling = Production Planning," "Advance expediting = Purchasing," and "Setup reduction & Multi-skilled workers = Manufacturing."
また用語問題として、「カムアップシステム(日付別のファイル・ボックスに伝票を入れ、納期数日前に自動的に浮き上がらせて事前督促する方式)」と「製造三角図(時間と数量で予定・着手・完成を三角形に表す図)」は名前と意味をそのまま覚えておきましょう。
For terminology questions, memorize the exact names and meanings of the "Come-Up System (placing slips in date-indexed pockets/boxes so they automatically surface several days before the due date for advance expediting)" and the "Manufacturing Triangle Chart (triangular time-vs.-quantity chart showing plan, start, and completion lines)."
さらにシステム用語の「MRP(部品表と在庫から所要量と発注時期を逆算)」「POP(現場実績のリアルタイム収集)」「VMI(納入業者主導の在庫補充)」の3つの区別も確実に押さえてください。
Also make sure you can distinguish the three system terms: "MRP (backward-calculating net requirements and order timing from BOM and inventory)," "POP (real-time collection of shop-floor actual results)," and "VMI (supplier-driven inventory replenishment)."
Key points
- 納期は「早ければ良い」わけではない!早期生産・早期納入は在庫増・資金圧迫・他製品の遅れを招く。
Delivery is NOT "the earlier, the better"! Early production and early delivery cause excess inventory, tied-up cash, and delays to other products. - カムアップシステム=日付別ポケットに伝票を保管し、納期前に自動的に浮き上がらせて督促漏れを防ぐ目で見る管理手法。
Come-Up System = visual control method storing order slips in dated pockets so they automatically surface before due dates to prevent missed follow-ups. - MRP=資材所要量計画/POP=生産時点情報管理(現場実績のリアルタイム把握)/製造三角図=時間×数量の三角形進捗グラフ。
MRP = Material Requirements Planning / POP = Point of Production (real-time shop-floor tracking) / Manufacturing Triangle Chart = Time × Quantity triangular progress graph.
| Word | Meaning |
|---|---|
| 早期納入の弊害 | harm of early delivery |
| 5部門(設計・計画・購買・製造・物流)の遅延対策 | delay countermeasures across 5 departments (Design, Planning, Purchasing, Manufacturing, Logistics) |
| カムアップシステムと製造三角図 | Come-Up System and Manufacturing Triangle Chart |
| MRP・POP・VMIの区別 | distinguishing MRP, POP, and VMI |
Delivery Management
Practice this chapter in the appOfficial references
- 中央職業能力開発協会(JAVADA) ビジネス・キャリア検定試験 3級 生産管理オペレーション 試験範囲 — https://www.javada.or.jp/jigyou/gino/business/subject.html
- 中央職業能力開発協会 編『ビジネス・キャリア検定試験 標準テキスト【専門知識】生産管理オペレーション 3級〔第4版〕』 — https://www.javada.or.jp/jigyou/gino/business/text.html